FBE Epoxy and Powder Coating: Reliable Protection for Industrial Applications

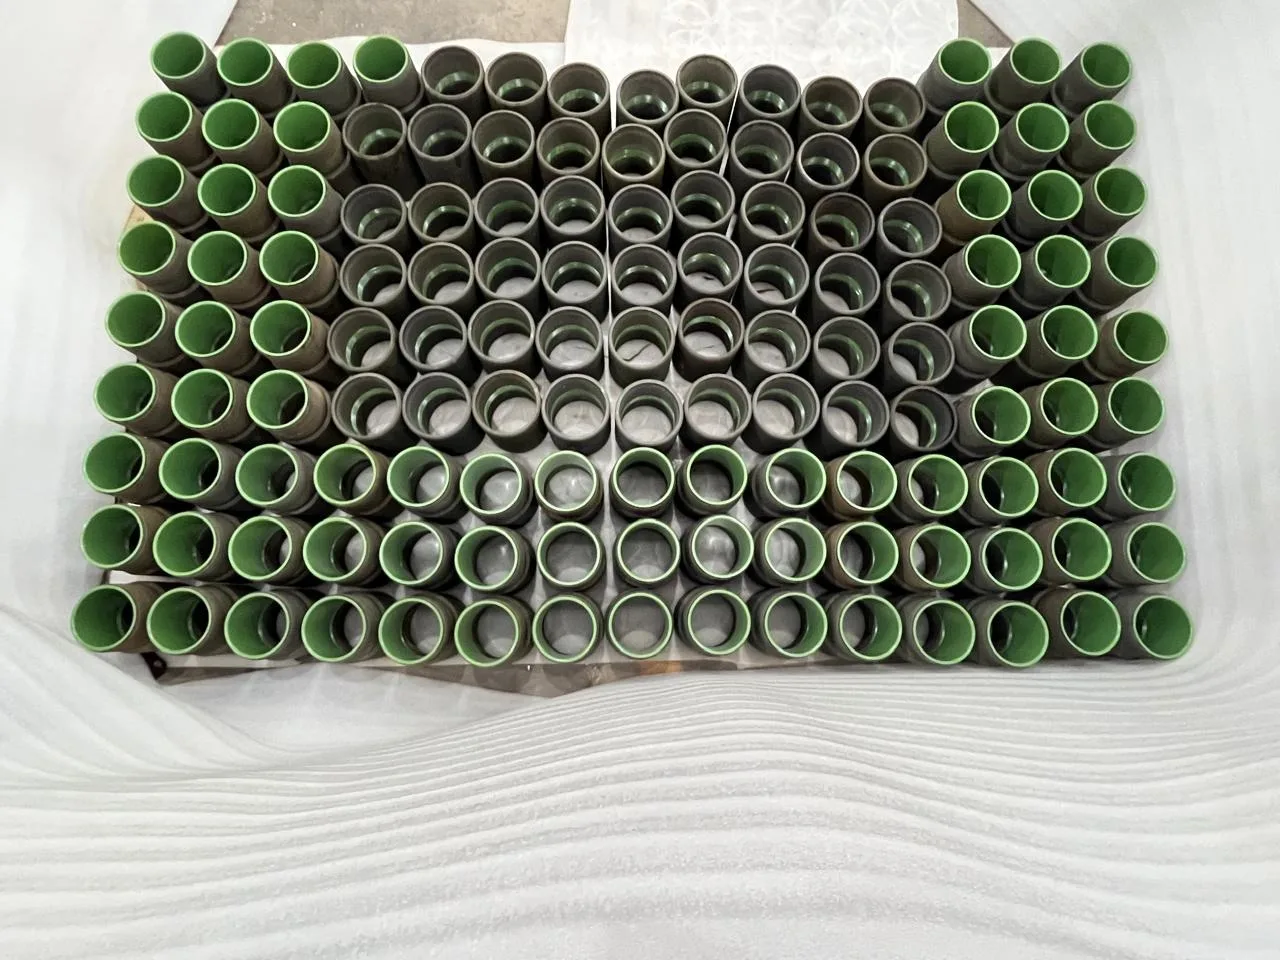
Industrial equipment, pipelines, and metal structures require strong protective coatings to withstand corrosion, moisture, chemicals, and changing environmental conditions. Choosing the right coating solution helps improve product durability, reduce maintenance requirements, and extend the working life of metal surfaces. FBE epoxy and powder coating technologies are widely used in industries where reliable surface protection and long-term performance are essential.
FBE, or Fusion Bonded Epoxy, is a high-performance coating system designed to protect metal surfaces from corrosion. It creates a strong bond with the prepared metal surface and forms a durable protective layer. This coating is commonly used in pipelines, water transportation systems, oil and gas infrastructure, and various industrial applications.
Understanding FBE Epoxy Coating
FBE epoxy is a thermosetting powder coating that provides excellent corrosion resistance and adhesion. It is applied to a properly prepared metal surface using an electrostatic spraying process. The coated component is then heated, allowing the powder to melt, flow, and cure into a continuous protective layer.
One of the major advantages of FBE epoxy is its ability to protect metal surfaces from rust and environmental damage. It offers good resistance to moisture, chemicals, and mechanical stress, making it suitable for demanding industrial environments. Its strong adhesion also helps maintain coating integrity during transportation, installation, and regular operation.
Industries prefer this coating because it provides dependable protection while supporting long-term operational efficiency. Proper surface preparation and controlled application are important for achieving consistent coating quality.
Importance of High-Quality FBE Powder
FBE powder plays an important role in determining the overall performance of a fusion bonded epoxy coating. The quality of the powder directly affects adhesion, coating thickness, curing behaviour, and resistance to corrosion. Therefore, selecting the right material is essential for industrial applications.
High-quality FBE powder is formulated to deliver uniform coverage and reliable performance. When applied under suitable conditions, it forms a smooth and durable coating that helps protect metal components against harsh operating conditions.
Different industrial requirements may demand different powder formulations. Factors such as operating temperature, exposure to chemicals, environmental conditions, and application methods should be considered before selecting a suitable product.
Manufacturers and industrial buyers should also focus on consistency, storage conditions, and application specifications to achieve the desired results. Using the correct FBE powder can help minimise coating defects and improve the service life of protected components.
Benefits of FBE Powder Coating
FBE powder coating is widely recognised for its protective properties and suitability for industrial applications. It offers several benefits that make it a preferred choice for metal protection.
1. Excellent Corrosion Resistance: FBE powder coating creates a protective barrier that prevents moisture and corrosive substances from directly affecting the metal surface.
2. Strong Adhesion: The coating bonds firmly with properly prepared metal, helping maintain protection during handling, installation, and service.
3. Long-Term Durability: Its resistance to environmental exposure and mechanical damage supports longer service life and reduces the need for frequent maintenance.
4. Chemical Resistance: Depending on the formulation, FBE coatings can withstand exposure to various industrial chemicals and challenging operating conditions.
5. Uniform Surface Protection: The application process helps create a consistent coating layer when appropriate equipment and curing conditions are maintained.
6. Industrial Versatility: FBE powder coating is suitable for pipelines, fittings, valves, metal components, and other equipment requiring dependable corrosion protection.
Applications Across Different Industries
FBE coatings are used in several industries because of their ability to protect metal components in demanding environments. In the oil and gas sector, they are commonly applied to pipelines and related infrastructure to help prevent corrosion. Water supply and wastewater treatment systems also benefit from protective coatings that improve the durability of metal pipes and fittings.
In addition, industrial manufacturing, chemical processing, and infrastructure projects use FBE coating solutions to protect different metal products. The coating selection depends on the operating environment, required performance standards, and intended application.
Choose Heatman Products for Industrial Coating Solutions
Selecting a reliable coating solution is an important decision for businesses that depend on durable metal components. Heatman Products focuses on industrial coating requirements and understands the importance of quality, performance, and product reliability.
Whether the requirement involves FBE epoxy, FBE powder, or advanced FBE powder coating solutions, choosing suitable materials and following proper application practices can make a significant difference in long-term results.
For industrial projects where corrosion protection and durability matter, investing in an appropriate FBE coating system is a practical way to protect valuable equipment and infrastructure. With the right coating selection, businesses can improve surface protection, minimise maintenance challenges, and support the long-term performance of their metal assets.
0 comments
Log in to leave a comment.
Be the first to comment.